Pressure Gauge Calibration Process | 18 Steps Every Technician Must Know (2026)
Pressure Gauge Calibration Process: What You Need to Know Before You Start

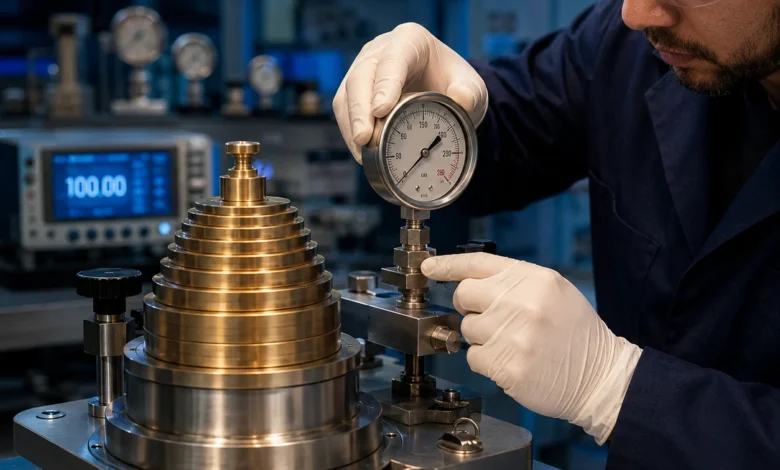
If you’ve ever handed a pressure gauge to a calibration technician and wondered exactly what happens next or if you’re the technician looking for a definitive, technically accurate guide that doesn’t gloss over the hard parts this is the article you need. I’ve been working in pressure calibration for years, and the one thing I consistently see is that most people either oversimplify the process or bury the practical steps under so much jargon that the actual procedure gets lost. I’m going to fix that here.
The pressure gauge calibration process is a structured, multi-step procedure that compares a gauge’s output against a traceable reference standard, documents any deviation between what the gauge reads and what the actual pressure is, and where deviation exceeds acceptable limits adjusts the gauge back into specification. That’s the short version. The full version involves understanding your gauge type, selecting the right calibration equipment, applying pressure correctly, recording as-found and as-left data, evaluating uncertainty, and documenting everything in a calibration certificate that satisfies your quality management system and regulatory requirements.
What this guide covers goes significantly beyond what you’ll find on most competitor sites. We’re going to walk through the complete calibration procedure step by step, explain the science behind concepts like hysteresis, linearity, repeatability, and the adiabatic effect, cover every major type of calibration equipment and when to use it, and answer the most common questions technicians and quality managers ask about pressure gauge calibration including where to find accredited labs and how to decide between on-site and off-site calibration services. Let’s get into it.
What Is a Pressure Gauge and Why Does the Calibration Process Matter?
Understanding the Instrument You’re Calibrating
Before you can calibrate a pressure gauge correctly, you need to understand what you’re working with. Pressure gauges measure the force that a fluid or gas exerts on a surface, expressed in units like PSI, bar, kPa, or inH₂O. They come in several fundamental types, and each type has its own calibration characteristics and failure modes.
An analog pressure gauge is the classic mechanical design it contains a bourdon tube, a curved metallic tube that straightens proportionally as internal pressure increases. That mechanical movement is transferred through a gear-and-lever mechanism to rotate a pointer across a calibrated dial. The accuracy of an analog gauge depends on the quality of its bourdon tube, the precision of its movement, and the correctness of its dial markings. Over time, the bourdon tube fatigues, the movement wears, and the pointer drifts which is exactly why the calibration process matters.
A digital pressure gauge replaces the mechanical movement with an electronic sensing element most commonly a piezoresistive sensor, which changes its electrical resistance in proportion to applied pressure. The sensor output is converted to a digital reading by an analog-to-digital converter and displayed on a numeric screen. Digital gauges are generally more accurate than analog gauges for the same price point, but they still drift as their electronic components age and as their sensor elements experience fatigue from pressure cycling.
A diaphragm pressure gauge uses a flexible diaphragm rather than a bourdon tube as the sensing element. This design is preferred in applications involving viscous, corrosive, or highly viscous media that would damage a bourdon tube. A differential pressure gauge measures the pressure difference between two points in a system, rather than pressure relative to atmosphere or absolute vacuum. These designs all require calibration, but the specific procedure and equipment selection differ based on type.
Why Pressure Gauge Calibration Cannot Be Optional
Every pressure gauge in industrial, pharmaceutical, healthcare, oil and gas, or food production service is making a measurement that someone or some automated system is using to make a decision. That decision might be whether a vessel is safe to operate, whether a batch has been processed at the correct pressure, or whether a pipeline is holding its specified test pressure. When the pressure gauge is out of calibration, every decision made based on its reading is built on incorrect data. The consequences range from wasted product and process failures to pressure vessel incidents and regulatory non-compliance.
Pressure gauges are also required to be calibrated under multiple regulatory frameworks: ISO 9001 quality management systems, ISO/IEC 17025 laboratory accreditation, FDA pharmaceutical regulations, API standards in the oil and gas sector, and ASME standards in pressure vessel applications. These aren’t administrative formalities they’re the regulatory recognition that pressure measurement integrity is a safety and quality requirement. If you’re looking for a deeper explanation of why calibration matters across all measurement types, the team at STS Calibration has covered the fundamentals of why calibration is important in detail.
What Are the Standard Steps in a Pressure Gauge Calibration Process?
The Complete 9-Step Calibration Procedure
This is the core of what you came here for. Here is the complete, technically accurate, step-by-step pressure gauge calibration process as it should be performed by a competent technician following best practices and ISO/IEC 17025 principles.
Step 1: Identify and Document the Gauge
Before applying any pressure, identify the gauge completely: manufacturer, model number, serial number, pressure range, accuracy class, and the process fluid it’s used with. Check the accuracy class this defines the permissible error, which is the maximum allowed deviation expressed as a percentage of full-scale range. A Class 1.0 gauge is permitted to deviate by up to 1.0% of its full-scale range. A Class 0.25 gauge allows only 0.25%. This determines how tight your calibration tolerance needs to be and what reference standard you need to use.
Step 2: Select the Correct Reference Standard
Your reference standard must be more accurate than the gauge you’re calibrating. The industry standard practice is a minimum test uncertainty ratio (TUR) of 4:1 meaning the calibration equipment’s uncertainty must be at least four times smaller than the gauge’s permissible error. If you’re calibrating a Class 1.0 gauge with a 0–100 PSI range, your permissible error is 1.0 PSI. Your reference standard must therefore have an uncertainty no larger than 0.25 PSI. Never skip this calculation using an insufficiently accurate reference standard invalidates the calibration.
Step 3: Inspect the Gauge Before Calibration
Before applying pressure, physically inspect the gauge. Check for cracked or moisture-contaminated dials, damaged Bourdon tubes, loose or bent pointers, corroded fittings, and any physical damage. A gauge with physical damage should be flagged for repair or retirement before calibration. Also confirm the gauge’s zero reading at atmospheric pressure a significantly off-zero reading before any calibration begins is your first data point and should be recorded.
Step 4: Set Up the Calibration Equipment
Assemble your calibration manifold the valve arrangement that allows you to apply pressure from your reference source to both the gauge under test and your reference standard simultaneously, and to vent pressure safely. Ensure all connections are leak-free. A pressure leak during calibration introduces dynamic pressure loss that corrupts your measurements. The reference standard and the gauge under test must be at the same elevation, or a correction must be applied for the hydrostatic head difference between them.
Step 5: Exercise the Gauge
Exercising the gauge means applying pressure to its full-scale range two or three times before taking any measurements. This process reduces the effects of mechanical friction and hysteresis in the gauge’s movement, allowing the mechanism to settle into its operating state. Skipping this step leads to artificially favorable initial readings that don’t represent the gauge’s true in-service performance. After exercising, return the gauge to zero and verify it reads correctly before proceeding.
Step 6: Apply Pressure and Record As-Found Data
Now you begin the actual measurement sequence. Apply pressure in incremental steps typically at 0%, 25%, 50%, 75%, and 100% of the gauge’s full-scale range, both on the upscale (increasing pressure) sequence and the downscale (decreasing pressure) sequence. At each point, use the dithering technique gently tap the gauge case to settle the pointer and eliminate the effect of pointer friction before recording the reading. Record the reference standard’s reading alongside each gauge reading. This complete dataset is your as-found data: the documented condition of the gauge before any adjustment.
Step 7: Evaluate the As-Found Data
Compare each gauge reading against the reference standard reading and calculate the deviation at each test point. Check these deviations against the gauge’s permissible error for its accuracy class. Also evaluate hysteresis the difference between the upscale and downscale readings at each test point and linearity whether the deviation follows a consistent pattern across the range or varies non-linearly. A gauge that exceeds its permissible error, shows excessive hysteresis, or exhibits non-linearity beyond its spec requires adjustment.
Step 8: Perform Zero and Span Adjustment
If adjustment is needed, perform zero and span adjustment. Zero adjustment corrects the gauge’s reading at the minimum point of its range (typically atmospheric pressure for a gauge pressure instrument). Span adjustment corrects the reading at the full-scale point. Most analog gauges have mechanical zero and span adjustments accessible through the gauge case. Digital gauges typically have electronic zero and span trim functions accessible through the instrument’s front panel or configuration interface. After adjustment, repeat the full upscale and downscale measurement sequence and record the results as your as-left data.
Step 9: Document and Issue the Calibration Certificate
Record all as-found and as-left data on the calibration record, note the reference standard used (including its identification number and its own calibration traceability), calculate and document the calibration uncertainty, and issue a calibration certificate. The certificate must include: gauge identification, calibration date, next due date, reference standard details, as-found and as-left data tables, measurement uncertainty statement, and the technician’s identification. File the certificate in your calibration records system and attach a calibration label to the gauge showing the calibration date and due date.
What Is the Standard Procedure for Calibrating a Pressure Gauge? The Technical Science Explained
The Pressure Comparison Method in Detail
The fundamental technique underlying all pressure gauge calibration is the pressure comparison method: you apply the same pressure to both the gauge under test (the device under test, or DUT) and your reference standard simultaneously, read both, and compare the results. The reference standard whether a deadweight tester, a precision digital reference gauge, or a pressure controller tells you what the actual pressure is. The DUT tells you what your gauge thinks the pressure is. The difference is the error.
This sounds simple, but in practice several physical factors complicate the comparison. The adiabatic effect is one of the most frequently overlooked sources of error in pressure calibration. When you rapidly increase pressure in a closed system as happens when you quickly pump up a hand pump calibrator the air or fluid compresses and its temperature increases temporarily. This temperature change causes a momentary density and pressure shift that affects your reading. To minimize adiabatic errors, always apply pressure slowly and allow the system to thermally stabilize before taking readings. This is especially important at higher pressures and with gas media.
Accuracy Class, Permissible Error, and Tolerance Limits
The accuracy class of a pressure gauge is its rated maximum error expressed as a percentage of full-scale range. Common accuracy classes for industrial gauges are 0.1, 0.25, 0.5, 1.0, 1.6, and 2.5. The accuracy class directly determines the permissible error the maximum allowable deviation at any point in the gauge’s range. For a 0–200 PSI gauge with an accuracy class of 1.0, the permissible error is 2.0 PSI at any point in the range.
Understanding this relationship is critical for calibration because it determines both the pass/fail criterion for the gauge and the minimum accuracy requirement for your reference standard. If your reference has an uncertainty comparable to the permissible error, your calibration is worthless you cannot determine whether a gauge that’s right at its tolerance limit is actually passing or failing, because your reference uncertainty overlaps with the tolerance band. This is why TUR ≥ 4:1 is the minimum professional standard, and TUR ≥ 10:1 is preferred for high-accuracy calibration work.
Stability, Drift, and the Calibration Interval Relationship
Stability refers to how well a gauge maintains its metrological properties over time. Drift is the gradual, usually unidirectional change in a gauge’s reading characteristics caused by material aging, elastic hysteresis in the bourdon tube, fatigue from pressure cycling, and environmental effects like temperature and vibration. Understanding a gauge’s drift behavior is essential for setting the correct calibration interval the maximum time allowed between calibrations.
The calibration interval should be set based on the gauge’s historical drift data, not just the manufacturer’s recommendation. If calibration records show that a particular gauge consistently drifts less than 30% of its permissible error between annual calibrations, the interval can potentially be extended. If it consistently drifts close to or beyond its permissible error within 12 months, the interval needs to be shortened. This data-driven approach to calibration interval management is one of the hallmarks of a mature calibration program and directly reduces both quality risk and calibration costs.
As-Found and As-Left Data: Why These Two Readings Define Your Entire Calibration
What As-Found Data Tells You About Your Gauge
The as-found condition of a gauge recorded before any adjustment is made is arguably the most important output of the entire calibration process. As-found data tells you whether the gauge was in or out of specification during its previous service period, how much it drifted since its last calibration, and whether your calibration interval is appropriate. If a gauge consistently comes in for calibration with significant as-found deviation, that’s a signal to shorten its calibration interval or investigate the cause of the drift whether it’s the operating environment, overpressure events, or end-of-life deterioration.
From a regulatory standpoint, as-found data is also the evidence you need for product release decisions. If a gauge is found out of calibration, any measurements made with it during the period since its last calibration are potentially invalid. Your quality system needs to have a documented process for assessing the impact of out-of-calibration instruments on product that was measured with them. The as-found record is the starting point for that impact assessment.
What As-Left Data Confirms About Your Adjustment
As-left data is recorded after all adjustments have been completed and the full measurement sequence has been re-run. It confirms that the adjustments brought the gauge within its permissible error across the full range, in both the upscale and downscale directions. The as-left data is what gets reported on the calibration certificate as the gauge’s current performance. It’s the data that auditors, regulators, and customers rely on when they trust your calibration documentation.
One important point: if a gauge cannot be adjusted to within specification because its bourdon tube has fatigued, its movement is worn, or its error is too large and non-linear to be corrected by simple zero and span adjustment the as-left data will still show out-of-tolerance results. In that case, the gauge must be removed from service, flagged as failed calibration, and either repaired or replaced. Issuing a calibration certificate for a gauge that cannot be brought within specification is a serious compliance and safety violation.
Understanding Accuracy, Hysteresis, Linearity, and Repeatability in Pressure Gauge Calibration
Hysteresis: The Difference Between Going Up and Coming Down
Hysteresis is the difference between a gauge’s reading at a given pressure point when approached from below (increasing pressure) versus from above (decreasing pressure). It exists in analog gauges because of friction and elastic behavior in the bourdon tube and movement mechanism the gauge doesn’t follow exactly the same path in reverse that it followed going forward. Hysteresis is evaluated by comparing upscale and downscale readings at each test point during the calibration sequence.
The maximum permissible hysteresis is typically half the total permissible error for the gauge’s accuracy class. A gauge with hysteresis that exceeds this limit is considered out of specification even if every individual upscale reading is within tolerance. In practice, significant hysteresis is often a sign that the gauge’s movement is worn or contaminated, or that the bourdon tube has developed a permanent set from overpressure. Identifying hysteresis in the as-found data helps you diagnose the root cause before deciding on repair or replacement.
Linearity: How Consistent Is the Error Across the Range?
Linearity describes whether the gauge’s error is consistent across its full measurement range, or whether it varies being within tolerance at some points and outside tolerance at others. A gauge with good linearity has a consistent, relatively flat error profile across the range. A gauge with poor linearity might read accurately at 50% of range but be significantly out of tolerance at 25% or 75%.
Linearity errors are evaluated by plotting the deviation at each calibration test point and assessing whether the deviations follow a linear pattern or curve. Non-linear errors are more difficult to correct with simple zero and span adjustment a span adjustment shifts the full-scale reading but doesn’t correct a non-linear deviation in the middle of the range. Gauges with significant non-linearity often require internal mechanical adjustment or replacement.
Repeatability: Can Your Gauge Be Trusted to Give the Same Answer Twice?
Repeatability is the ability of a gauge to give the same reading when the same pressure is applied multiple times under identical conditions. It’s measured by applying a specific test pressure multiple times and recording each reading. The spread of those readings typically expressed as the range or standard deviation quantifies the gauge’s repeatability. A gauge with poor repeatability is fundamentally unreliable, regardless of whether its average reading is accurate, because you can’t trust any individual reading it provides.
Repeatability errors in analog gauges are usually caused by friction in the movement, a loose pointer, or contamination in the mechanism. In digital gauges, they can be caused by electronic noise in the sensor circuitry or signal conditioning. Repeatability is one of the components that contributes to the overall measurement uncertainty of a calibrated gauge and must be accounted for in the uncertainty budget of the calibration.
What Are the Common Types of Calibration Equipment for Pressure Gauges?
The Four Main Pressure Calibration Equipment Categories
This is one of the most common questions I get from technicians entering the pressure calibration field, and it’s one where getting the answer wrong leads directly to invalid calibrations. The choice of calibration equipment depends on the pressure range being calibrated, the accuracy class of the gauge, the working environment (lab versus field), and the available budget. Here are the four main categories and when to use each.
Deadweight Tester The Primary Standard
The deadweight tester is the primary pressure standard for calibration. It works by generating a known pressure through the gravitational force exerted by calibrated masses placed on a precision piston-cylinder assembly. The pressure it generates is calculated from the formula P = F/A force (mass × gravitational acceleration) divided by piston area. Because the mass values and piston area are known with very high accuracy, a deadweight tester can generate pressures with uncertainties as low as 0.005% of reading, making it the most accurate portable pressure reference available.
Deadweight testers are the reference of choice for calibrating high-accuracy pressure gauges, pressure transmitters, and transfer standards. They are cumbersome for field use but are standard in metrology laboratories and high-quality on-site calibration setups. They require regular maintenance the piston-cylinder assembly must be kept clean, and the masses must themselves be calibrated against traceable weight standards.
Hand Pump Calibrator The Field Workhorse
The hand pump calibrator is a portable, manually operated pressure source that allows a technician to generate and hold pressure while simultaneously reading a reference standard and the gauge under test. It’s the most commonly used tool for routine field calibration of industrial pressure gauges because it’s portable, inexpensive, and doesn’t require external power or compressed gas supplies.
Hand pump calibrators are available in hydraulic (oil or water filled) and pneumatic (air) versions. Hydraulic types can generate significantly higher pressures than pneumatic types hydraulic hand pumps can reach 70,000 PSI or more, while pneumatic types are typically limited to a few hundred PSI. The limitation of hand pump calibrators is precision they require a skilled, careful technician to apply pressure slowly and stably, and their output is subject to adiabatic effects if pressure is applied too quickly. They are best suited for gauges with accuracy classes of 0.5 and above.
Pressure Controller / Electronic Calibrator Automated Precision
A pressure controller or electronic pressure calibrator is an automated instrument that generates, controls, and stabilizes a set pressure electronically. Modern pressure calibrators combine a pressure generation system, a precision reference sensor, and a digital interface into a single unit. They can apply pressure to a programmed sequence of test points automatically, hold each point stable for a set time, and record the DUT reading making them ideal for high-volume calibration environments.
Multi-function pressure calibrators also include electrical measurement capabilities, allowing them to simultaneously calibrate pressure transmitters measuring the 4–20mA output of the transmitter while applying calibrated pressure input. These instruments represent the current state of the art for industrial pressure calibration and are central to automated calibration software integration in modern calibration management systems. For laboratories performing high volumes of calibrations, the investment in a pressure controller pays back quickly in reduced calibration time and improved consistency.
Test Pump with Reference Gauge The Budget Option
A test pump paired with a high-accuracy reference gauge is the simplest and lowest-cost calibration setup. The test pump provides a regulated pressure source, and the reference gauge a recently calibrated, high-accuracy instrument with a known uncertainty serves as the reference standard in place of a deadweight tester. This setup is appropriate for calibrating low-accuracy class gauges (Class 1.0 and above) in applications where the TUR requirement can be met with a good-quality reference gauge.
The limitation of this approach is the reference gauge’s accuracy a reference gauge calibrated to 0.1% full scale can only support calibration of gauges with permissible errors ≥ 0.4% (maintaining TUR ≥ 4:1). For higher-accuracy gauges, a deadweight tester or electronic pressure calibrator is required.
Deadweight Tester vs. Hand Pump vs. Pressure Controller: Choosing the Right Equipment
Matching Equipment to Application Requirements
The choice between calibration equipment types isn’t just about what’s available it’s a technical decision that directly affects the validity of your calibration. Here’s a practical framework for making that choice correctly.
Use a deadweight tester when: you’re calibrating gauges with accuracy classes of 0.1 or 0.25, you need the lowest achievable calibration uncertainty, you’re calibrating primary reference standards or transfer standards, or your ISO/IEC 17025 accreditation scope requires primary standard calibration capability.
Use a hand pump calibrator when: you’re doing field calibration of industrial gauges with accuracy class 0.5 or worse, portability is a priority, the gauge range is within the pump’s capability, and the application doesn’t justify the cost and complexity of electronic calibration equipment.
Use a pressure controller when: you’re calibrating large volumes of gauges or transmitters, you need to calibrate electronic pressure transmitters alongside mechanical gauges, you want to integrate calibration data with automated software, or you need the precision and stability of automated pressure control for accuracy classes better than 0.5.
The calibration manifold regardless of which pressure source you use is the essential plumbing component that connects everything together. A properly designed manifold allows you to isolate the supply pressure from the test system, vent the system safely, connect multiple gauges simultaneously, and control the pressurization sequence with precision. Never attempt pressure gauge calibration without a proper manifold improvised connections with standard fittings are a safety hazard and a source of leaks that corrupt calibration data.
Analog Pressure Gauge Calibration: Bourdon Tube Mechanics and Zero & Span Adjustment
How the Bourdon Tube Behaves Under Calibration Conditions
The bourdon tube is the heart of every analog pressure gauge, and understanding its behavior is essential for performing calibration correctly and interpreting calibration results accurately. The bourdon tube is a curved or coiled metallic tube typically C-shaped or helical that is sealed at one end and connected to the pressure inlet at the other. When pressure is applied internally, the tube tends to straighten, and this deflection is mechanically amplified and transferred to the pointer through a gear-and-lever linkage called the movement.
The relationship between applied pressure and bourdon tube deflection is designed to be linear meaning equal increments of pressure should produce equal increments of pointer rotation. In practice, slight non-linearities exist because of variations in tube geometry, movement friction, and the geometry of the gear linkage. These non-linearities are what you’re measuring and evaluating when you record data at the 25%, 50%, and 75% range points during calibration.
The bourdon tube is also the primary failure point in an analog gauge’s lifespan. Repeated pressure cycling causes elastic fatigue, gradually changing the tube’s stiffness and shift its zero point. Exposure to overpressure even briefly can cause permanent plastic deformation, fundamentally altering the gauge’s calibration across its entire range. This is why overpressure history is an important question to ask before calibrating a gauge that has been in demanding service.
Zero and Span Adjustment Techniques for Analog Gauges
Zero adjustment on an analog gauge is typically performed by repositioning the pointer on its shaft, or by adjusting a mechanical zero-set screw accessible through the gauge face. The goal is to make the pointer read exactly zero (or the minimum scale value) at the gauge’s reference pressure (atmospheric for gauge pressure instruments, or a defined low pressure for other types).
Span adjustment corrects the gauge’s reading at full scale. On most analog gauges, span is adjusted by changing the effective length of the movement link arm the lever that connects the bourdon tube tip to the gear train. Increasing the effective arm length increases the span (the pointer moves more for a given pressure change); decreasing it reduces the span. Getting both zero and span right simultaneously is an iterative process adjusting span changes the reading at mid-range, which may require a zero re-check. Experienced technicians develop a feel for how many iterations are needed, but the process always ends with a full verification run through all test points after adjustment.
Digital Pressure Gauge Calibration: Electronic Methods and Sensor Trim Procedures
Calibrating Piezoresistive Sensors in Digital Gauges
The piezoresistive sensor used in most digital pressure gauges measures pressure by detecting the change in electrical resistance of a silicon strain gauge bridge as it deforms under applied pressure. The sensor output is a small voltage signal proportional to pressure, which is amplified and converted to a digital reading by the gauge’s electronics. Calibration of a digital gauge involves verifying and correcting this signal chain at defined pressure points.
Digital gauge calibration typically involves two electronic trim functions: zero trim (correcting the reading at zero pressure) and span trim (correcting the reading at full-scale pressure). These adjustments are made through the gauge’s front panel menu or through a configuration interface, and they modify internal calibration coefficients stored in the gauge’s non-volatile memory. The procedure is cleaner and faster than analog gauge adjustment, but it requires careful attention to the sequence always zero before span, and always verify with a full upscale/downscale run after both adjustments.
An important consideration in digital gauge calibration is temperature sensitivity. Most piezoresistive sensors have some temperature coefficient their output changes slightly with temperature even at constant pressure. High-quality digital gauges include internal temperature compensation circuitry that corrects for this effect, but this compensation is only accurate within the gauge’s specified temperature range. Calibration should always be performed within the gauge’s rated temperature range, and calibration certificates should note the ambient temperature at the time of calibration.
Differential and Diaphragm Pressure Gauge Calibration: Special Considerations
Calibrating Differential Pressure Gauges
Differential pressure gauge calibration is more complex than gauge pressure calibration because the instrument has two pressure ports high side and low side and measures the difference between them. Calibration requires applying controlled pressure differentials across the two ports while keeping both ports within the instrument’s working pressure limits. A calibration manifold for differential pressure work must include provisions for pressurizing both the high and low side independently, equalizing pressure across both ports for zero checks, and venting each side safely.
The key calibration check unique to differential gauges is the overpressure test: applying the gauge’s rated static pressure to both sides simultaneously (equalized) to verify that the gauge reads zero and is not damaged. Many differential gauges can handle high line pressures as long as the differential across the diaphragm stays within range but applying the full line pressure to only one side can rupture the diaphragm. Always check the gauge’s static pressure rating before proceeding.
Diaphragm Gauge Calibration in Corrosive Service
Diaphragm pressure gauges used in corrosive or viscous media applications require special handling during calibration because the process side of the gauge cannot be exposed to standard calibration fluid. These gauges are often filled with a neutral fluid (glycerin, silicone oil) between the diaphragm and the bourdon tube or sensor element. Calibration must be performed using the appropriate compatible fluid on the process side, or using a dry calibration technique that pressurizes only the gauge side of the instrument.
For gauges that have been in corrosive service, the diaphragm condition must be inspected before calibration. A corroded, pitted, or deformed diaphragm affects linearity and hysteresis and may indicate the gauge is beyond reliable calibration. In these cases, the instrument should be retired rather than calibrated and returned to service, as a compromised diaphragm represents a process fluid containment risk. For help evaluating diaphragm gauge serviceability, the STS Calibration team offers on-site inspection and calibration services for process instrumentation across all gauge types.
Test Uncertainty Ratio (TUR) and Test Accuracy Ratio (TAR): The Numbers That Define Calibration Quality
Understanding TUR and Why 4:1 Is the Minimum Standard
The test uncertainty ratio (TUR) is the ratio of the gauge’s tolerance (permissible error) to the calibration standard’s measurement uncertainty. It quantifies the confidence with which you can determine whether the gauge is actually in or out of specification. A TUR of 4:1 means the reference’s uncertainty is one-fourth of the gauge’s permissible error there is enough separation between what the reference can resolve and what the gauge’s tolerance allows for you to make a statistically reliable pass/fail decision.
When TUR falls below 4:1, you enter a zone called the “guardband region” the area near the tolerance limits where measurement uncertainty from the reference itself makes it impossible to reliably classify the gauge as passing or failing. For example, if your gauge’s permissible error is 1.0 PSI and your reference has an uncertainty of 0.5 PSI (TUR = 2:1), a gauge reading 0.8 PSI off its reference could actually be anywhere from 0.3 PSI to 1.3 PSI out right at the tolerance limit, or significantly outside it. You simply can’t tell. In high-stakes applications, guardbanding techniques must be applied when TUR is less than 4:1, which reduces the effective tolerance window to compensate for reference uncertainty.
TAR vs. TUR: A Common Confusion Resolved
The test accuracy ratio (TAR) is an older concept still used by some organizations that expresses the ratio of the reference standard’s accuracy specification (not uncertainty) to the DUT’s permissible error. The distinction matters because accuracy specifications are worst-case limits, while uncertainty is a statistically derived quantity based on actual measurement analysis. TUR using uncertainty is the more rigorous and scientifically correct metric, and it is the one required by ISO/IEC 17025 and ANSI/NCSL Z540.3. If your calibration supplier quotes you TAR values without TUR analysis, ask specifically for the measurement uncertainty of the standards they use and calculate your own TUR. This is a basic quality check that separates credible calibration services from unreliable ones.
Traceability, ISO/IEC 17025, and NIST: The Regulatory Framework Behind Valid Calibration
What NIST Traceability Actually Means for Pressure Calibration
NIST traceability is a phrase that appears on nearly every calibration certificate, but its meaning is frequently misunderstood. Traceability to NIST (National Institute of Standards and Technology) means there is an unbroken, documented chain of calibration comparisons linking your gauge’s calibration all the way back to NIST’s primary pressure standards the pressure measurement standards that NIST maintains at the highest accuracy level achievable by any laboratory in the United States.
Each link in the traceability chain involves a calibration comparison with documented uncertainty. Your field gauge is calibrated against a transfer standard. That transfer standard is calibrated against a laboratory reference. The laboratory reference is calibrated by an accredited laboratory whose own standards have been calibrated by or compared to NIST. At each step, the uncertainty increases as it propagates from the primary standard down to the field instrument which is exactly why TUR requirements exist to ensure that enough accuracy margin remains at each level. For pressure calibrations performed outside the US, traceability to equivalent national metrology institutes (PTB in Germany, NPL in the UK, NMIJ in Japan) provides equivalent scientific validity.
ISO/IEC 17025 Accreditation and What It Guarantees
ISO/IEC 17025 is the international standard for testing and calibration laboratory competence. An ISO/IEC 17025 accredited calibration laboratory has been independently assessed by a recognized accreditation body in the US, this is typically A2LA (American Association for Laboratory Accreditation) or NVLAP (National Voluntary Laboratory Accreditation Program) and has demonstrated that its calibration processes, technical staff, equipment, and quality management system meet the standard’s requirements.
What ISO/IEC 17025 accreditation guarantees for your pressure gauge calibration:
- The laboratory’s reference standards are calibrated, traceable, and maintained to documented uncertainty specifications
- The calibration procedures used are technically validated and documented
- The technical staff performing calibrations are competent and assessed
- The calibration certificates issued include measurement uncertainty
- The laboratory participates in proficiency testing to verify its measurement consistency against peer laboratories
When you need pressure gauge calibration certificates that will withstand regulatory inspection FDA audits, ISO 9001 certification audits, API compliance assessments accredited calibration under ISO/IEC 17025 is the only documentation that carries sufficient authority. The STS Calibration laboratory provides ISO/IEC 17025 accredited calibration services with full NIST-traceable documentation for pressure gauges across all accuracy classes and pressure ranges.
Calibration Interval: How Often Should a Pressure Gauge Be Calibrated?
Setting the Right Calibration Frequency for Your Application
The calibration interval the maximum time allowed between calibrations for a given instrument is one of the most practically important decisions in managing a pressure gauge fleet. Set it too long and you risk instruments drifting out of specification during service. Set it too short and you waste calibration budget without improving measurement reliability.
The starting point for any calibration interval decision is the manufacturer’s recommendation, which is typically 12 months for most industrial pressure gauges. But the manufacturer’s recommendation is a generic starting point, not an application-specific answer. The correct interval for a specific gauge in a specific application depends on: the severity of the operating environment (temperature extremes, vibration, pulsating pressure), the frequency of use, the criticality of the measurement, the gauge’s historical drift data from previous calibrations, and the regulatory requirements of the industry.
Gauges in harsh environments high-cycle pressure service, elevated temperature, corrosive media, significant vibration typically need calibration intervals of 3–6 months. Gauges in stable, light-duty service with low criticality may support 18–24 month intervals without measurable risk. The only way to know which category your gauges fall into is to analyze their historical as-found calibration data and look at how much they actually drift between calibrations. This analysis is a core function of a well-run calibration management program.
Regulatory Requirements for Calibration Interval
In regulated industries, the calibration interval isn’t always a free decision it may be specified by the applicable standard or regulation. FDA pharmaceutical manufacturing regulations typically require annual calibration as a minimum. API standards for oil and gas instrumentation specify intervals based on the instrument’s criticality classification. ASME standards for pressure vessel testing specify calibration requirements for test gauges used in pressure testing. Always cross-check your internally set calibration interval against the regulatory requirements of your specific industry and application.
For organizations managing large instrument fleets, a calibration scheme that classifies instruments by criticality and assigns different intervals to different criticality classes is far more efficient than applying a single interval to all instruments. STS Calibration offers calibration program consulting to help organizations develop optimized calibration schemes that balance risk management with cost efficiency.
Where Can I Find Accredited Labs for Pressure Gauge Calibration Services?
How to Identify a Credible Accredited Calibration Laboratory
Finding a legitimate, accredited calibration lab for pressure gauge calibration requires checking more than just a website’s claims. Any laboratory can claim to provide “traceable” or “accredited” calibration the only way to verify it is to check the laboratory’s accreditation scope directly with the accreditation body that issued it. In the US, you can search A2LA’s online directory (a2la.org) or NVLAP’s directory (nvlap.nist.gov) and look up any laboratory’s specific scope of accreditation. The scope document specifies exactly which measurement quantities, ranges, and uncertainty levels the laboratory is accredited for. A laboratory accredited for pressure calibration from 0–10,000 PSI with an uncertainty of 0.01% FS is a credible choice for calibrating most industrial pressure gauges in that range.
Questions to ask before choosing a calibration lab:
What is your ISO/IEC 17025 accreditation number and which body issued it? A credible lab will give you this information immediately and without hesitation.
What is the measurement uncertainty of your pressure calibration standards at the range I need? The answer must support a TUR ≥ 4:1 for your gauge’s accuracy class.
Do you provide as-found and as-left data on calibration certificates? Any lab that only reports as-left data is hiding the as-found condition which is a red flag for quality system compliance.
How long is your calibration turnaround time, and do you offer expedited service? Turnaround time directly affects your instrument’s availability, and a quality lab should be transparent about its lead times.
Do you offer on-site calibration services? For large instrument fleets or production-critical gauges that can’t be removed from service easily, on-site calibration is a significant operational advantage.
STS Calibration: Accredited Pressure Gauge Calibration Services
STS Calibration provides ISO/IEC 17025 accredited pressure gauge calibration services for industrial, pharmaceutical, oil and gas, aerospace, and laboratory applications. Our laboratory is equipped with primary deadweight tester standards, high-accuracy electronic pressure calibrators, and automated calibration documentation systems that deliver full as-found and as-left data on every calibration certificate. We service analog pressure gauges, digital pressure gauges, differential pressure gauges, diaphragm gauges, and pressure transmitters across pressure ranges from vacuum to 70,000 PSI. We also provide on-site calibration services for facilities that need calibration performed at the point of use without instrument removal.
On-Site Calibration Services vs. Sending to a Lab: Which Is Right for Your Operation?
The Business Case for On-Site Pressure Gauge Calibration
On-site calibration services where a calibration technician brings calibrated reference equipment to your facility and performs calibrations at your location offer significant operational advantages for many organizations. The primary benefit is eliminating the downtime and logistical burden of removing gauges from service, packaging and shipping them to a lab, waiting for the calibration cycle, and reinstalling them. For production-critical processes where a gauge cannot be removed without shutting down a process line, on-site calibration is often the only practical option.
On-site calibration also provides an opportunity for technicians to observe the gauge in its installed context noting whether there are process conditions (vibration, temperature, pulsating pressure) that are likely to accelerate drift and require a shortened calibration interval. This contextual insight is something that lab-based calibration, with no visibility into the operating environment, cannot provide.
When a Laboratory Calibration Is the Better Choice
Laboratory calibration is the better choice when your gauges require the highest-accuracy calibration available particularly for gauge accuracy classes of 0.1 or 0.25, which require primary standard (deadweight tester) calibration in controlled laboratory conditions that are difficult to replicate in the field. Laboratories also offer better environmental control (temperature, humidity, vibration isolation) that is necessary for the most precise calibration work.
For most organizations managing mixed fleets of gauges some high-accuracy, some routine industrial a combination approach works best: routine industrial gauges calibrated on-site for operational efficiency, and high-accuracy or critical gauges sent to the accredited laboratory for primary standard calibration. The STS Calibration team provides both services and can help you develop a hybrid calibration strategy that optimizes cost, turnaround time, and measurement integrity.
Temperature Sensor, Flow Meter, and Medical Equipment Calibration: How Pressure Calibration Connects
Temperature Sensor Calibration Guide: The Parallel Process
The temperature sensor calibration process follows the same fundamental logic as pressure gauge calibration comparison against a traceable reference standard, recording of as-found and as-left data, evaluation against tolerance limits, and documentation on a calibration certificate. For temperature sensors (thermocouples, RTDs, thermistors), the reference standard is typically a precision platinum resistance thermometer (PRT) or a calibrated reference thermocouple, and the calibration medium is a dry block calibrator or liquid bath that provides a stable, uniform temperature environment.
Just as pressure gauges drift due to bourdon tube fatigue and movement wear, temperature sensors drift due to material changes in the sensing element. RTDs drift because of strain relief in the platinum element and contamination. Thermocouples drift because of chemical changes in the thermocouple wire junction. The calibration process for temperature sensors is therefore an essential companion to pressure calibration in any comprehensive instrument management program. For facilities managing both types of instruments, combining pressure and temperature calibration visits reduces logistical overhead and total calibration cost significantly.
Flow Meter Calibration Procedure: Pressure Calibration’s Close Cousin
The flow meter calibration procedure has a direct relationship to pressure calibration because many flow measurement technologies differential pressure flow meters like orifice plates, venturis, and pitot tubes depend on differential pressure measurement as their fundamental operating principle. The flow calculation derives the volumetric flow rate from the measured differential pressure across a flow element using a known mathematical relationship. If the differential pressure gauge or transmitter used in that measurement is out of calibration, the flow calculation is wrong even if the flow element itself is perfectly good.
This interdependency means that a proper flow meter calibration program must include calibration of the associated pressure instrumentation as an integral step. Organizations that calibrate their flow meters but neglect the differential pressure transmitters driving the flow calculation are not getting the benefit they expect from their calibration investment.
Medical Equipment Calibration Requirements: Pressure Calibration in Healthcare
Medical equipment calibration requirements for pressure-measuring devices are among the most stringent in any sector. Ventilators, anesthesia machines, infusion pumps, autoclaves, and blood pressure monitoring equipment all incorporate pressure measurement as a safety-critical function. The FDA’s Quality System Regulation (21 CFR Part 820) requires documented calibration of all measuring and test equipment used in medical device manufacturing. Hospitals and clinical facilities are governed by CLIA requirements and Joint Commission standards, which mandate regular calibration and performance verification for all diagnostic and therapeutic equipment with measurement functions.
Pressure gauge calibration in medical settings requires ISO/IEC 17025 accredited calibration with full traceability documentation, shorter calibration intervals reflecting the patient safety stakes, and calibration procedures that follow device-specific standards (IEC 60601 series for medical electrical equipment, ISO 10993 for biocompatibility). The calibration certificates issued must be retained as part of the device’s maintenance records and must be available for inspection during regulatory audits. The stakes in medical equipment calibration are not abstract they are directly tied to patient outcomes, and the consequences of calibration failures in this sector are correspondingly serious.
How to Build a Preventive Maintenance and Calibration Program for Pressure Gauges
Integrating Calibration Into Your Preventive Maintenance Strategy
The most effective pressure gauge calibration programs aren’t standalone activities they’re integrated into the facility’s broader preventive maintenance framework. This integration means calibration due dates are tracked in the same system as other maintenance activities (typically a Computerized Maintenance Management System or CMMS), calibration results feed into equipment reliability analyses, and out-of-calibration findings trigger the same corrective action workflow as other maintenance failures.
When calibration is integrated with preventive maintenance, the full picture of instrument health becomes visible. A gauge that consistently shows high as-found deviation, exhibits increasing hysteresis over successive calibrations, and has a history of exposure to overpressure events is an instrument that your maintenance data will flag as a replacement candidate before it fails in service and causes a production or safety incident. This predictive insight is one of the highest-value outputs of a well-managed calibration program.
Building Your Calibration Interval Optimization Process
A mature calibration program uses as-found data systematically to optimize calibration intervals. The process works like this: after each calibration, record the as-found deviation as a percentage of the gauge’s permissible error. Over multiple calibration cycles, plot this data to see the drift trend. If the gauge consistently returns with as-found deviation less than 50% of its permissible error, it’s a candidate for interval extension. If it frequently returns with deviation close to or exceeding its permissible error, the interval needs to be shortened.
This data-driven approach to interval management often called “calibration interval optimization” or “dynamic interval adjustment” is recognized and encouraged by ISO/IEC 17025, ISO 9001, and ILAC guidelines. It’s the only scientifically defensible basis for setting calibration intervals, and it typically results in significant reductions in total calibration cost by extending intervals for stable instruments while focusing resources on instruments that actually need more frequent attention.
FAQs
What are the standard steps in a pressure gauge calibration process?
The standard steps are: identify and document the gauge, select a reference standard with TUR ≥ 4:1, inspect the gauge physically, assemble the calibration manifold, exercise the gauge by cycling pressure three times, apply pressure at defined test points in both increasing and decreasing sequences while recording as-found data, evaluate deviations against permissible error, perform zero and span adjustment if needed, record as-left data, and issue a calibration certificate with full traceability documentation.
What is the standard procedure for calibrating a pressure gauge?
The standard procedure uses the pressure comparison method: a traceable reference standard and the gauge under test are connected simultaneously to a common pressure source via a calibration manifold. Pressure is applied in steps from 0% to 100% of range (upscale) and from 100% back to 0% (downscale). At each step, dithering is applied to the gauge and both the reference and gauge readings are recorded. Deviations are calculated and compared to the gauge’s permissible error for its accuracy class.
Where can I find accredited labs for pressure gauge calibration services?
Search the A2LA directory (a2la.org) or NVLAP directory (nvlap.nist.gov) by measurement discipline (pressure) and location. Verify that any laboratory you consider is specifically accredited for the pressure range and accuracy level you need, and that their measurement uncertainty supports a TUR ≥ 4:1 for your gauges. STS Calibration provides ISO/IEC 17025 accredited pressure gauge calibration for a wide range of industrial and precision applications.
What are the common types of calibration equipment for pressure gauges?
The four main types are: deadweight testers (highest accuracy, primary standards used for accuracy class 0.1 and 0.25 gauges), hand pump calibrators (portable, field-use for accuracy class 0.5 and above), electronic pressure controllers/calibrators (automated, high-volume, suitable for transmitter calibration), and test pumps paired with high-accuracy reference gauges (economical setup for routine industrial calibration).
What is the test uncertainty ratio (TUR) and why does it matter?
TUR is the ratio of the gauge’s permissible error to the calibration standard’s measurement uncertainty. A TUR ≥ 4:1 is the minimum requirement for valid calibration it ensures that the reference is accurate enough to reliably determine whether the gauge is passing or failing its tolerance. A TUR below 4:1 means the reference’s own uncertainty overlaps with the gauge’s tolerance band, making pass/fail determinations statistically unreliable.
How often should a pressure gauge be calibrated?
The correct calibration interval depends on the gauge’s operating environment, usage intensity, accuracy class, historical drift data, and regulatory requirements. The manufacturer’s recommendation (typically 12 months) is the starting point, but the actual interval should be set based on analysis of the gauge’s as-found calibration history. Gauges in harsh environments may need 3–6 month intervals; stable, light-duty gauges may support 18–24 months. Always verify against your industry’s regulatory requirements.
What happens if a pressure gauge fails calibration?
If a gauge fails calibration (as-found deviation exceeds permissible error or cannot be adjusted within tolerance), it must be immediately removed from service and tagged as out of calibration. A calibration failure response must be initiated: assess all measurements made with the gauge since its last calibration, determine which decisions were based on those measurements, and evaluate whether any product, process, or safety impact occurred. The gauge must then be either repaired and re-calibrated or replaced.
What is the difference between as-found and as-left data?
As-found data is recorded before any adjustment, it shows the gauge’s condition as it was during its previous service period. As-left data is recorded after adjustment, it shows the gauge’s condition when returned to service. Both sets of data must appear on the calibration certificate. As-found data is essential for impact assessment when a gauge is found out of calibration.
Conclusion
After walking through the complete process from gauge identification and equipment selection through as-found data recording, zero and span adjustment, TUR analysis, ISO/IEC 17025 compliance, and calibration interval management I want to leave you with a clear perspective: pressure gauge calibration is not a compliance checkbox. It is a precision engineering process that directly determines whether the pressure data driving your industrial decisions is trustworthy.
Every step in the procedure exists for a reason grounded in measurement science. Exercising the gauge eliminates friction artifacts. Recording as-found data before adjustment preserves the evidence needed for quality system decisions. Maintaining TUR ≥ 4:1 ensures your pass/fail determinations are statistically valid. Documenting full traceability creates the defensible audit trail that regulators and customers require. None of this is bureaucracy it is the professional discipline that separates reliable pressure measurement from guesswork.
If your current calibration program needs strengthening whether you’re building a program from scratch, optimizing your calibration intervals, or looking for an accredited laboratory that provides real technical value rather than just paper certificates STS Calibration is ready to help. Our team brings deep pressure calibration expertise, ISO/IEC 17025 accredited laboratory capability, and on-site calibration services to industrial facilities across all sectors.
Written by the STS Calibration technical team, specialists in pressure, temperature, electrical, and dimensional calibration with over two decades of hands-on metrology experience across manufacturing, pharmaceutical, aerospace, and energy industries.
Also Read:
- Calibration Guide 2026 | Process, Steps & Accuracy
- 20 ways | How To Fix Android Phone Touch Screen Problem |
- CRITICAL Fixes PS5 Controller Not Working | STS-Calibration
- How to Calibrate Equipment Correctly | 15 Critical Steps Most Technicians Miss
- Calibration vs Standardization | 15 Key Differences Explained
- What is Calibration? Why Accuracy Fails Without It